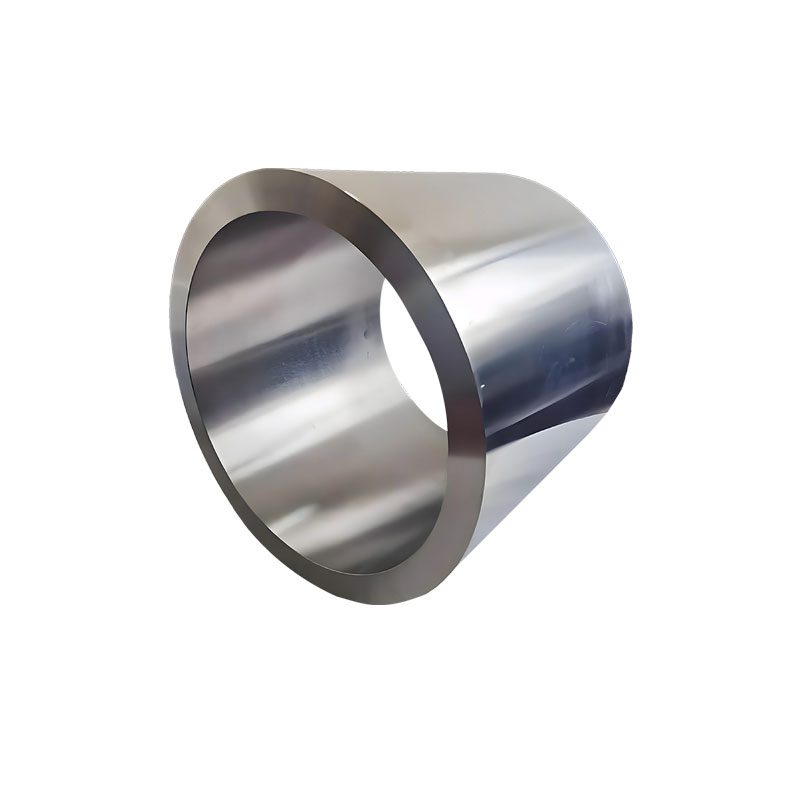
Seamless rolled rings up to 7.5 m outside diameter, IT7–IT9 tolerance.
| Outside diameter | Up to 7,500 mm |
|---|---|
| Inside diameter | From 101.6 mm |
| Height / thickness | 10–1000 mm |
| Tolerance | IT7–IT9 rolled; machined to drawing |
| Standards | GB/T 16598-2013, ASTM B381 (Ti), ASTM A473 / A788 (stainless), ASTM A388 (UT) |
| Delivery state | As-rolled, annealed, normalised, Q+T, or rough/finish machined |
A rolled ring is forged with the grain running circumferentially, all the way round, with no weld and no seam. For bearing races, valve bodies, flanges-turned-from-ring and pressure-vessel nozzles, that continuous grain is why the part survives fatigue.
Upset, punch and ring-roll — radial and axial rolling controls both wall and height, which is how we hold diameter tolerance to ±0.3 mm on precision rings.
Material utilisation above 80% because the ring is formed close to final section rather than cut from plate.
Outside diameter from a few tens of millimetres to 7.5 m; height from 10 mm to 1000 mm.
Tolerance IT7–IT9 as rolled; tighter after machining.
UT to GB/T 6402 or ASTM A388, with the acceptance level agreed before forging.
Dimensional report with a full ring map for large diameters.
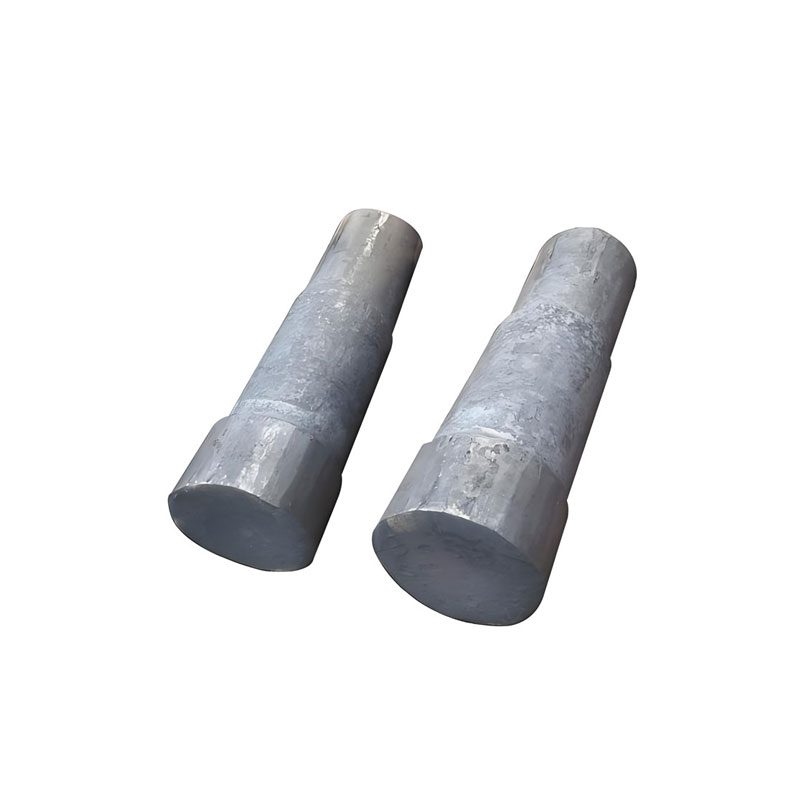
Forged round bar Φ80–Φ1200 mm, forging ratio ≥4:1, UT to GB/T 6402 or ASTM A388.
Specifications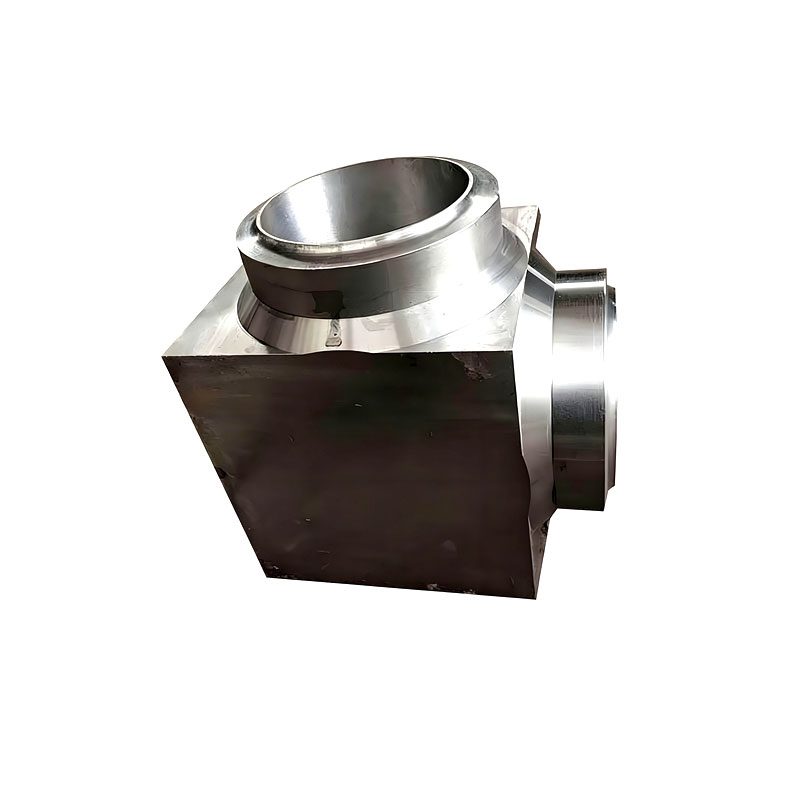
Forged square billet 40–1000 mm, dense core, for dies, tools and machined blocks.
Specifications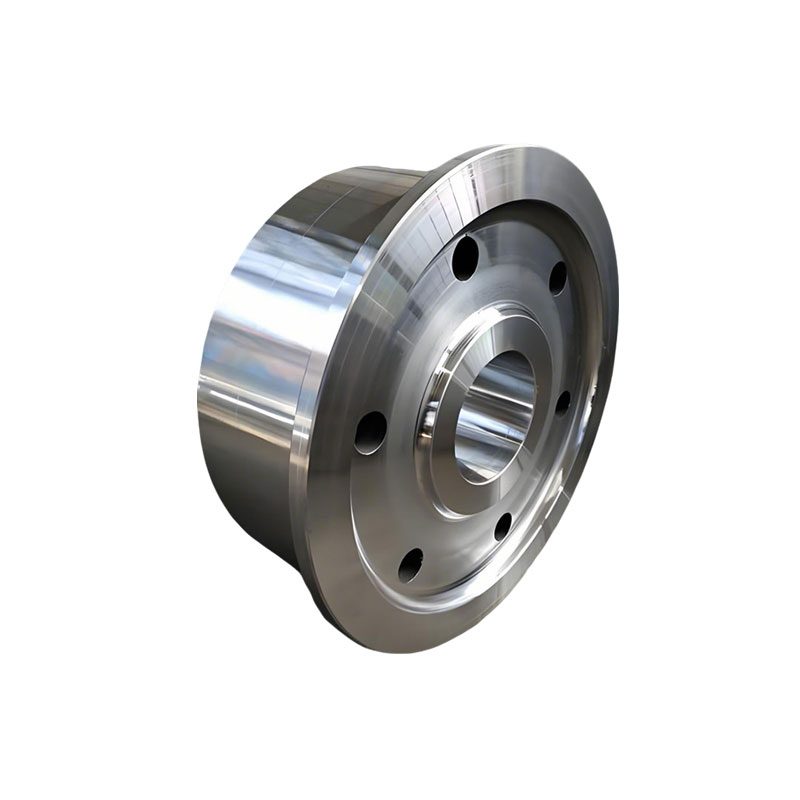
Non-standard forgings to drawing — complex profiles, thin walls, tight tolerances.
SpecificationsQuotes within one business day. Send grade, size, pressure class, face type and quantity — a drawing works better than a description.